
Fire protection water storage is a critical consideration for food production facilities, where protecting people, production infrastructure, equipment and inventory requires a dependable supply of water for fire suppression systems.
At a food production plant in Rhome, Texas, SBS Tanks USA recently supplied a 159,030-gallon SBS Tanks ST15R07 fire protection water storage tank designed to provide the required water supply for the facility’s sprinkler system. While the primary purpose of the tank is fire protection, the project incorporates another important consideration: rainwater harvesting.
Working in partnership with SBS Tanks dealer, Rainwater Equipment, the project brought fire protection water storage and rainwater collection together within a single engineered tank solution. The tank was designed to meet the usable capacity requirements of the sprinkler system while incorporating an inlet for harvested rainwater.
Food production facilities have a particular need for reliable fire protection infrastructure. Production areas, processing equipment, electrical systems, packaging materials, storage and other critical assets can all contribute to the complexity of protecting a modern manufacturing environment.
For the Rhome facility, the requirement was straightforward but essential: provide a dedicated water storage tank capable of supplying the plant’s sprinkler system.
The project was designed around NFPA 22, the Standard for Water Tanks for Private Fire Protection. Compliance with NFPA 22 is an important consideration when designing and supplying a tank for a dedicated fire protection application, ensuring that the storage system is engineered around the requirements of the associated fire protection system.
But the project also presented an opportunity to consider how the fire protection tank could contribute to a broader water-management strategy.
Rainwater harvesting is becoming an increasingly relevant consideration for commercial and industrial developments. Large facilities can have substantial roof areas capable of collecting significant volumes of rainfall, creating an opportunity to capture and store water that would otherwise run off the site.
At Rhome, this consideration was incorporated directly into the fire protection tank design.
The rainwater harvesting inlet allows collected rainfall to be directed into the storage tank, providing an additional source of water to the tank while maintaining its primary role as fire protection storage.
Combining these functions within one tank can offer practical advantages where a facility has both fire protection storage requirements and an interest in capturing rainwater. It allows the water storage strategy to be considered as part of the facility’s overall design.
The approach also reflects a broader shift toward more responsible water management across commercial and industrial facilities. Rainwater harvesting, backup water storage and water recycling are increasingly being considered alongside conventional water supplies as businesses look for ways to improve water security and manage available resources.
The Rhome project demonstrates how these considerations can be incorporated without compromising the fundamental purpose of a fire protection water tank.
The tank supplied for the project was an ST15R07, part of the SBS Tanks Standard Range (https://sbstanksusa.com/).
The Standard Range provides modular steel water storage solutions across a broad range of capacities, allowing tank configuration to be matched to the requirements of individual commercial and industrial projects.
For the Rhome project, the ST15R07 provided the required 159,030-gallon capacity within a configuration suited to the facility and its fire protection requirements.
The modular construction of SBS Tanks allows tanks to be manufactured, transported and assembled efficiently on site, providing flexibility for projects where water storage requirements, available space and site conditions vary.
This flexibility is particularly useful for industrial facilities, where water storage requirements can be determined by building size, occupancy, fire protection design, available space and local engineering criteria.
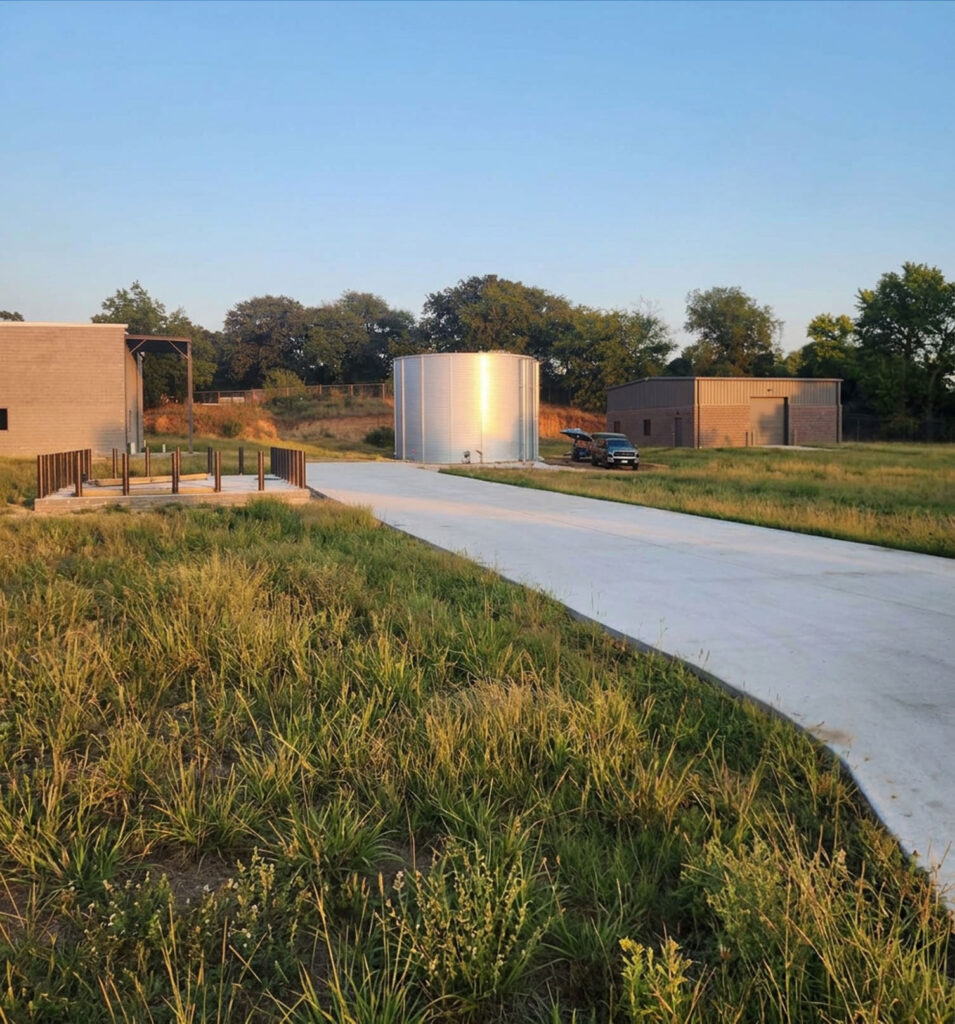
The design process for the Rhome tank included an independent review by a Texas-licensed professional engineer.
The engineer simulated the applicable loading conditions, analyzed the tank structure and stamped and certified the final plans. Specific attention was also given to the integration of the rainwater harvesting element into the tank design.
This independent engineering review formed an important part of the project’s quality and compliance process. Fire protection water storage is not simply a matter of selecting a tank with the required volume. The tank and associated infrastructure must work together as an engineered system.
The project also followed established SBS Tanks manufacturing and installation procedures, supported by manufacturing under an ISO 9001 quality-management system.
Preparation of the tank foundation was completed by the contractor ahead of installation, allowing the foundation to be ready for the first day of tank assembly. This preparation helped the installation proceed efficiently and according to plan.
The installation was completed successfully, with the contractor and end user satisfied with the professionalism and efficiency of the installation process.
The completed installation provided the facility with the dedicated fire protection water storage required for its sprinkler system while incorporating the additional rainwater harvesting capability into the overall water storage solution.
The Rhome project illustrates an important principle in industrial water storage: a tank does not necessarily need to serve only one purpose.
The primary requirement for this facility was reliable fire protection water storage. That requirement remained central throughout the engineering and design process, with the tank developed to meet NFPA 22 requirements and the usable capacity required by the sprinkler system.
At the same time, incorporating a rainwater harvesting inlet provided an opportunity to make the storage infrastructure part of a wider water-management strategy.
For food production facilities, manufacturing plants and other large commercial developments, these considerations are increasingly relevant. Water availability, responsible consumption, resilience and fire protection all have a role to play in the design of modern industrial infrastructure.
The Rhome installation brings these requirements together in a practical, engineered solution: a 159,030-gallon ST15R07 fire protection water storage tank with a rainwater harvesting inlet, designed specifically around the needs of the facility.
No two industrial water storage projects are identical. Capacity requirements may be determined by a fire protection system, while available space, site conditions, local engineering requirements and additional water-management objectives can all influence the final design.
For the Rhome food production plant, the solution was developed around two complementary objectives—providing dependable water storage for fire protection while incorporating the ability to harvest rainwater.
The result is a tank designed not simply to store water, but to support the wider operational requirements of the facility.
As industrial developments continue to place greater emphasis on water security and responsible resource management, integrating complementary functions into purpose-designed storage infrastructure provides another way to approach these challenges.
The Rhome project demonstrates how fire protection water storage can be engineered around the specific requirements of a modern food production facility—providing the capacity required for sprinkler protection while creating an additional opportunity to capture and store rainwater.
SBS Tanks is a global water storage solutions provider specializing in the design, manufacture and installation of modular bolted steel tanks. With applications across industries including fire protection, utilities, mining, agriculture, commercial, rainwater harvesting and industrial water storage, SBS Tanks provides engineered storage solutions designed around the specific requirements of each project.
Our modular tank technology provides flexibility in capacity, configuration and installation, while our project delivery approach incorporates engineering, manufacturing and on-site installation.
From fire protection water storage to rainwater harvesting and other water infrastructure requirements, SBS Tanks works with customers, contractors, engineers and industry partners to deliver reliable water storage solutions for a wide range of applications.
To learn more about SBS Tanks USA and our water storage solutions, visit www.sbstanksusa.com.
© SBS Holdings 2026
